Warning: preg_match(): Compilation failed: non-hex character in \x{} (closing brace missing?) at offset 52 in /www/wwwroot/dzxinmi.com/wp-content/plugins/xy-assistant/includes/class-xya-write.php on line 1374
Warning: preg_match(): Compilation failed: non-hex character in \x{} (closing brace missing?) at offset 49 in /www/wwwroot/dzxinmi.com/wp-content/plugins/xy-assistant/includes/class-xya-write.php on line 1374
Warning: preg_match(): Compilation failed: non-hex character in \x{} (closing brace missing?) at offset 46 in /www/wwwroot/dzxinmi.com/wp-content/plugins/xy-assistant/includes/class-xya-write.php on line 1374
Warning: preg_match(): Compilation failed: non-hex character in \x{} (closing brace missing?) at offset 43 in /www/wwwroot/dzxinmi.com/wp-content/plugins/xy-assistant/includes/class-xya-write.php on line 1374
Warning: preg_match(): Compilation failed: non-hex character in \x{} (closing brace missing?) at offset 40 in /www/wwwroot/dzxinmi.com/wp-content/plugins/xy-assistant/includes/class-xya-write.php on line 1374
Warning: preg_match(): Compilation failed: non-hex character in \x{} (closing brace missing?) at offset 37 in /www/wwwroot/dzxinmi.com/wp-content/plugins/xy-assistant/includes/class-xya-write.php on line 1374
Warning: preg_match(): Compilation failed: non-hex character in \x{} (closing brace missing?) at offset 34 in /www/wwwroot/dzxinmi.com/wp-content/plugins/xy-assistant/includes/class-xya-write.php on line 1374
Warning: preg_match(): Compilation failed: non-hex character in \x{} (closing brace missing?) at offset 31 in /www/wwwroot/dzxinmi.com/wp-content/plugins/xy-assistant/includes/class-xya-write.php on line 1374
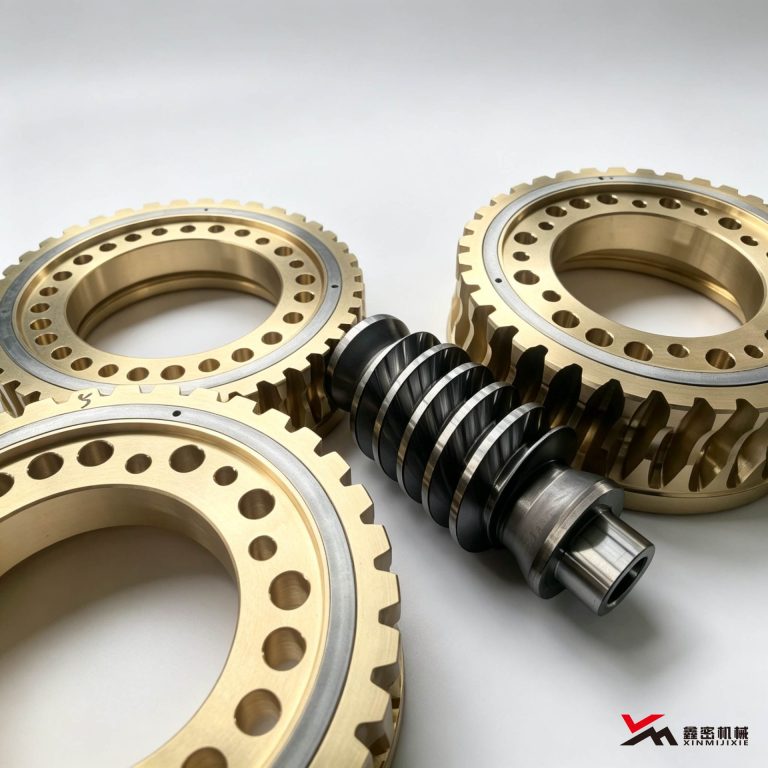
蜗轮蜗杆副的精度、耐磨性与使用寿命,主要由加工工艺和品控流程决定。同一规格的产品,不同厂家的工艺路线不同,成品质量差异往往很明显。下面按工序拆解精密蜗轮蜗杆的标准化加工流程与关键质量控制点,供采购和设备工程师参考。
一、原材料甄选与预处理
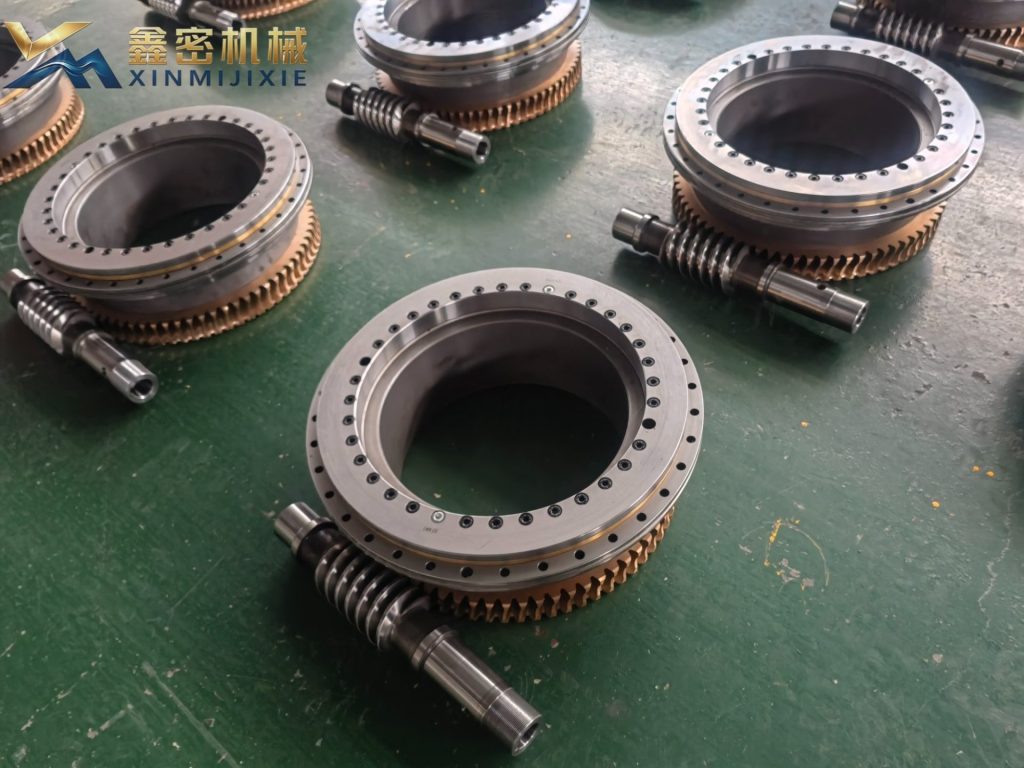
蜗轮常用高纯度锡青铜或铝青铜,蜗杆常用 40Cr 等合金结构钢。材料进场后应先做成分与硬度检验,排除裂纹、夹渣、硬度不达标等问题,从源头避免使用回收料或劣质坯料。
二、粗加工成型
用数控车床完成外圆、端面、台阶等基础加工,控制尺寸公差,并为后续滚齿、磨齿工序预留合理加工余量,防止精加工阶段变形。
三、滚齿加工
采用数控滚齿机加工齿形,控制模数、齿高、齿距、压力角等参数,保证齿形规整、啮合准确。蜗轮副的啮合质量直接影响传动的平稳性与噪音水平,是整条工艺链的核心工序。
四、热处理
蜗杆一般做调质并配合表面淬火,提高齿面硬度与芯部韧性,兼顾耐磨和抗疲劳;蜗轮青铜件进行稳定化处理,消除加工内应力,防止后期变形开裂。
五、磨齿
高精度蜗轮蜗杆通常经过磨齿,以修正热处理变形、去除齿面毛刺、优化齿形与齿向精度,可明显降低传动噪音、减小回程间隙,提升设备定位精度。
六、检测与出厂质检
成品需检测尺寸公差、齿形误差、齿向误差、侧隙、同轴度、硬度等指标,全部达标后方可出厂。
| 工序 | 主要设备 | 质量控制点 |
|---|---|---|
| 粗加工 | 数控车床 | 外圆/端面公差、加工余量 |
| 滚齿 | 数控滚齿机 | 模数、齿距、压力角、齿形 |
| 热处理 | 调质+淬火设备 | 表面硬度、芯部韧性 |
| 磨齿 | 磨齿机 | 齿形/齿向精度、表面质量 |
| 检测 | 三坐标/齿形仪等 | 公差、侧隙、同轴度、硬度 |
小厂与正规厂的工艺差异
部分小作坊为降低成本会简化工序,例如省略磨齿、简化热处理、原材料不检测、无成品质检,容易导致齿面粗糙、精度差、噪音大、寿命短。全流程加工与全流程质检,是保证批量产品一致性的基础。
关于德州鑫密机械
德州鑫密机械是蜗轮蜗杆及减速机生产企业,具备数控精车、滚齿、磨齿、热处理与检测等工序的自主加工能力,支持标准件与非标定制。如需选型或定制,可联系其技术团队沟通设备工况与精度要求。